How to Choose a PCB Manufacturing and Assembly Partner?

Choosing a PCB manufacturing and assembly partner can determine whether a product reaches the market smoothly or stalls during production. The right partner must offer more than attractive quotes. It should demonstrate process control, engineering depth, transparent communication, and verified capacity. This matters as electronics supply chains remain exposed to material shortages, labor constraints, and shifting demand. IPC’s 2024 Electronics Industry Sentiment Survey highlights continuing pressure from costs, availability, and workforce challenges. These pressures can quickly affect component sourcing, production schedules, and final quality.

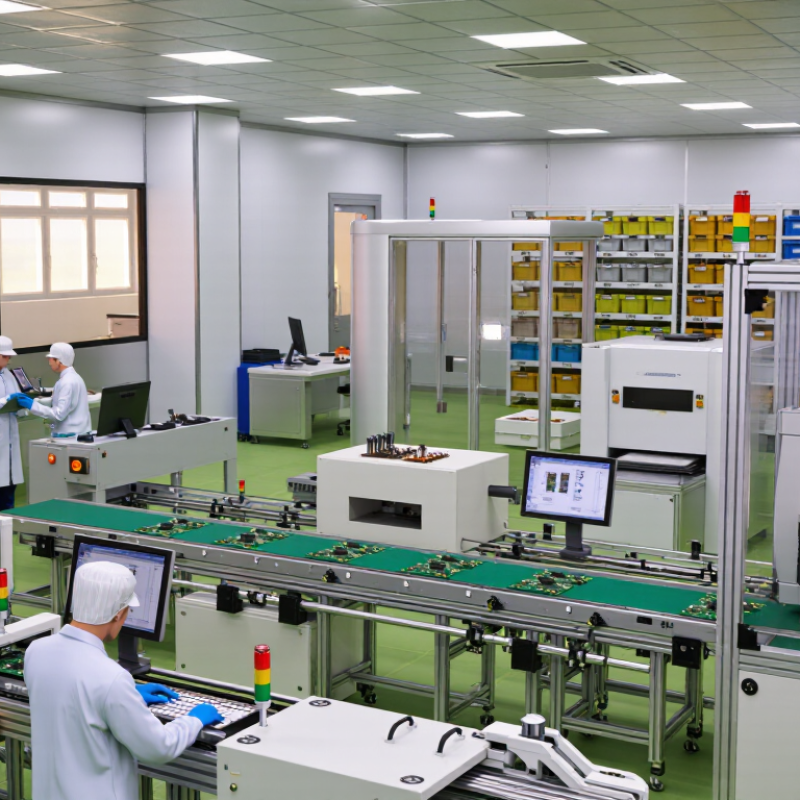
A reliable evaluation should examine the complete pcb manufacturing and assembly process. Ask for evidence of design-for-manufacturing reviews, controlled material storage, solder-paste inspection, AOI, X-ray inspection, and functional testing. Factory records should show traceability from incoming components to finished boards. Certifications such as ISO 9001, UL recognition, and relevant IPC workmanship standards add useful assurance, but certificates alone are not enough. Request recent audit summaries, sample inspection reports, defect data, and realistic capacity figures. Prismark’s PCB industry research continues to show the scale and competitiveness of the global PCB market, making supplier differentiation increasingly important. Price is only one variable.

A strong partner also supports prototypes, engineering changes, and stable volume production. Clarify minimum order quantities, tooling ownership, approved substitutes, and escalation procedures before signing. Visit the facility when possible. Observe humidity controls, operator training, and how nonconforming boards are isolated. No partner is perfect. A polished presentation can still hide weak execution. Therefore, score each supplier against measurable evidence, not promises, and leave room for reassessment after the first production run.
How to Choose a PCB Manufacturing and Assembly Partner?

Define Your PCB Manufacturing and Assembly Requirements

Choosing a PCB manufacturing and assembly partner starts with a precise requirement sheet.

Define board size, layer count, material, copper weight, and controlled impedance targets. State annual volume and prototype quantity separately. A five-board prototype needs different support than 50,000 production units. Include component package types, smallest pitch, and assembly technology. Will the design use through-hole parts, surface-mount parts, or both? Specify testing needs, such as automated optical inspection, in-circuit testing, or functional testing. Small omissions become expensive later.

Share fabrication files, schematic data, pick-and-place files, bill of materials, and revision history. Confirm acceptable substitutions before production begins. For each component, record its part number, lifecycle status, tolerance, and approved alternatives.

Ask how the partner manages moisture-sensitive devices, electrostatic protection, and traceability. These details reveal practical experience better than polished sales claims. Request sample inspection reports and certificates relevant to your market. Check whether their process follows recognized quality systems and documented change control. Evidence matters.

Set measurable delivery and quality requirements. Define target yield, defect classification, packaging, labeling, and shipment conditions. Agree on who approves engineering changes and how delays are reported.

I once treated delivery time as the main requirement; that choice ignored inspection and rework capacity. The schedule looked good on paper. It failed during component shortages. A better plan leaves room for substitutions, testing, and one realistic production review. Your requirement sheet may still be incomplete. Let manufacturing engineers challenge it early, before costs become difficult to reverse.

Evaluate Technical Capabilities and Production Capacity

How to Choose a PCB Manufacturing and Assembly Partner?

A capable PCB partner should match your design, not merely advertise advanced equipment. Ask whether the factory regularly produces your layer count, board thickness, copper weight, and surface finish. For high-speed designs, confirm controlled-impedance testing and material traceability. For dense layouts, inspect experience with microvias, fine-pitch components, and HDI structures.

Request evidence, not promises.

Review sample inspection reports, process-control plans, and first-article records. Reliable facilities typically combine AOI, automated X-ray inspection, solder-paste measurement, and electrical testing. Their engineers should explain DFM findings clearly before production begins. Certification matters, but practical records reveal more. Ask how they control humidity, component storage, oven profiles, and lot identification.

Production capacity requires equal attention. A factory may have impressive monthly output but limited capacity for your board type. Ask about available SMT lines, shift patterns, changeover time, and peak-season loading. Confirm whether assembly and bare-board production are managed under compatible schedules. Check recent on-time delivery data, not only standard lead times. A realistic partner should describe bottlenecks openly and provide a recovery plan for delays.

Do not overlook scaling.

A pilot run of 100 boards proves little about a stable run of 10,000. Ask how the partner maintains feeder accuracy, replenishes components, and preserves test coverage during volume increases. No manufacturing process is perfect. I would also challenge unclear yield figures, because attractive percentages can hide rework. A site audit, technical review, and small trial order often expose problems earlier than a polished presentation.

Verify Quality Standards, Certifications, and Testing Processes

A reliable PCB manufacturing and assembly partner should prove quality through records, not polished promises. Ask for current certificates, their scope, issuing body, and expiration date. ISO 9001 supports controlled processes, but it does not guarantee perfect boards. The certificate must cover the actual production site.

Review the partner’s inspection flow in detail. Automated optical inspection can detect missing parts, solder bridges, and placement errors. X-ray inspection helps examine hidden joints beneath packages. Electrical testing should include flying-probe, in-circuit, or functional testing when suitable. For high-speed boards, request impedance reports and test coupons. These details reveal whether testing matches your design risks.

Traceability matters when a defect appears months later. Lot codes should connect materials, operators, machines, inspection results, and rework records. Ask how nonconforming boards are isolated and how corrective actions are verified. A good supplier can show anonymized reports, sample first-article records, and calibration certificates. Visit the facility if possible. Observe handling, storage humidity, and cleanliness. Small habits often expose larger weaknesses.

Do not accept every certificate at face value. Some documents may be valid but irrelevant to your product. I have learned that a complete checklist can still miss poor communication during engineering changes. Request a sample change-control record and ask who approves deviations. The answer may reveal more than the audit folder.

How to Choose a PCB Manufacturing and Assembly Partner? — Verify Quality Standards, Certifications, and Testing Processes
Evaluation Area What to Verify Relevant Standards or References Objective Evidence to Request Recommended Acceptance Criteria Priority
Quality Management System Whether documented procedures control design transfer, purchasing, production, inspection, nonconforming products, corrective actions, and records. ISO 9001:2015 quality management system requirements.
  • Current certificate and scope
  • Recent surveillance or recertification status
  • Quality manual or process map
  • Corrective-action procedure
The certificate scope should cover the actual PCB fabrication and assembly activities required for the project. Procedures should be controlled and traceable. High
Medical or Regulated Production Whether the partner has a quality system appropriate for products requiring additional regulatory controls. ISO 13485:2016, where medical-device manufacturing activities apply.
  • Certificate with applicable scope
  • Device-history or production-record examples with sensitive information removed
  • Risk-management and change-control procedures
Use a partner whose certified scope and documented controls match the intended product, market, and regulatory responsibilities. High when applicable
PCB Fabrication Quality Control of board construction, materials, dimensions, copper features, plating, solder mask, silkscreen, and workmanship. IPC-6012 for rigid printed boards; IPC-A-600 for printed board acceptability.
  • Fabrication capability statement
  • Material and laminate certificates
  • Cross-section reports
  • Dimensional and visual inspection records
Finished boards should meet the agreed IPC class, drawing tolerances, layer stack-up, surface-finish requirements, and approved fabrication notes. High
Assembly Workmanship Quality of component placement, solder joints, cleanliness, markings, polarity, mechanical assembly, and rework. IPC-A-610 for electronic assembly acceptability; J-STD-001 for soldered electrical and electronic assemblies.
  • Workmanship standards used on the production floor
  • Operator training and certification records
  • First-article inspection report
  • Sample defect photographs or inspection criteria
The assembly should meet the customer-defined IPC class and documented soldering, component-placement, cleanliness, and marking requirements. High
Component Authenticity and Traceability Ability to control approved manufacturers, date codes, lot numbers, moisture-sensitive devices, substitutes, and counterfeit risk. Customer-approved bill of materials, component-storage requirements, and documented purchasing controls.
  • Full material traceability records
  • Approved-vendor and substitution procedure
  • Receiving-inspection records
  • Moisture-sensitive-device handling logs
No component substitutions should occur without written approval. Lot and date-code information should remain traceable from receipt through finished assembly. High
Automated Optical Inspection Whether automated optical inspection checks solder paste, component presence, polarity, placement, solder joints, and visible defects. Inspection criteria defined by IPC-A-610 and the approved assembly documentation.
  • AOI coverage list
  • Program-generation and revision-control process
  • False-call and escape-rate data
  • Defect images linked to board or lot identification
AOI should be used as a controlled inspection step, with human review of flagged defects and documented handling of inspection escapes. High
X-Ray Inspection Capability to inspect hidden solder joints and internal structures, especially bottom-terminated, array-package, or densely populated assemblies. Inspection limits and workmanship requirements agreed in the assembly quality plan.
  • X-ray inspection capability and sample images
  • Inspection coverage and sampling plan
  • Void, bridging, open-joint, and alignment criteria
Use X-ray inspection when hidden solder joints cannot be adequately evaluated by optical methods. Criteria should be defined before production approval. Medium to High
Electrical Testing Verification that nets, components, programmed devices, and functional interfaces operate according to the approved design. Customer-approved test specifications, test fixtures, and controlled software revisions.
  • In-circuit test or flying-probe test coverage
  • Functional-test procedure
  • Test limits and calibration records
  • Pass/fail reports linked to serial number or lot
Testing should cover the failure modes important to the product. Test programs, limits, fixtures, and results must be revision-controlled and traceable. High
Bare-Board Electrical Testing Verification of continuity, isolation, and unintended shorts before assembly. Customer netlist, fabrication drawing, and agreed electrical-test requirements.
  • Flying-probe or fixture-test method
  • Test coverage statement
  • Continuity and isolation limits
  • Test records for each panel or lot
Every required net should be tested using an approved method, with test results retained according to the project record-retention requirement. High
Cleanliness and Contamination Control Control of ionic residues, flux residues, particles, handling contamination, and cleaning-process effectiveness. J-STD-001 cleanliness requirements and customer-defined cleanliness limits; applicable ionic contamination test methods.
  • Cleaning-process description
  • Ion chromatography or equivalent test reports, where required
  • Cleanliness sampling plan
  • ESD and handling procedures
Cleanliness limits should be defined for the product environment. Results must remain within the agreed limits, particularly for high-impedance or high-reliability circuits. Medium to High
Environmental and Reliability Testing Ability to evaluate performance under temperature, humidity, vibration, shock, cycling, or operating-life conditions when required. Customer product specification and applicable environmental test methods, such as IEC 60068 series methods.
  • Qualification and validation reports
  • Equipment calibration certificates
  • Test profiles and acceptance limits
  • Failure-analysis and corrective-action records
Test profiles should represent the product’s intended operating and storage environment. Acceptance limits and sample quantities should be approved before testing. Medium when applicable
ESD and Moisture Control Protection of sensitive components and assemblies during receiving, storage, handling, assembly, and shipment. ANSI/ESD S20.20 for an ESD control program; J-STD-033 for handling moisture-sensitive devices.
  • ESD control-plan summary
  • Daily wrist-strap and workstation checks
  • Humidity and floor-control records
  • Moisture-barrier-bag and bake-control records
ESD controls should be implemented in designated areas, verified routinely, and supported by documented training and inspection records. High
Calibration and Measurement Control Whether inspection, testing, and measurement equipment remains accurate and suitable for its intended use. ISO 9001 measurement-resource controls and traceable calibration practices.
  • Calibration certificates
  • Equipment asset list
  • Due-date and out-of-tolerance procedure
  • Reference standards and environmental controls
Critical equipment should have current calibration status, defined intervals, traceable standards, and documented actions for out-of-tolerance conditions. High
Nonconformance and Corrective Action How defects are contained, analyzed, corrected, verified, and prevented from recurring. Documented nonconformance, root-cause, corrective-action, and change-control procedures.
  • Redacted corrective-action reports
  • Root-cause analysis examples
  • Containment and effectiveness checks
  • Defect-trend reports
Defects should be recorded by type and lot, affected material should be contained, root cause should be evidence-based, and corrective actions should include effectiveness verification. High
Final Documentation and Release Completeness and control of inspection, test, material, traceability, deviation, and shipment records. Customer quality agreement and the partner’s controlled-record procedures.
  • Certificate of conformance template
  • Final inspection and test reports
  • Material and lot-traceability records
  • Approved deviation records
Product should not be released until required inspections and tests are complete, results are acceptable, and all deviations have written approval. High

Compare Pricing, Lead Times, Communication, and Supply Chain Support

Choosing a PCB manufacturing and assembly partner requires more than comparing the lowest quotation. I have seen a cheaper bid become expensive after tooling changes, missing components, and repeated engineering questions. Ask for an itemized price covering fabrication, assembly, testing, setup, and freight. Hidden charges matter.

Lead time should be measured from approved files, not from the first inquiry. Request separate dates for prototype boards, component purchasing, assembly, and inspection. A reliable partner explains what happens if a key component becomes unavailable. Supply chain support should include approved alternatives, current stock checks, and clear material traceability. Ask for evidence, not optimistic promises.

Communication often reveals operational maturity. During one project, daily updates looked impressive, but technical answers arrived too late. That assumption was wrong. A useful partner confirms receipt of your files, identifies risks, and records design changes in writing. Ask whether you will have one accountable contact and how urgent issues are escalated. Review sample inspection reports, quality certifications, and corrective-action records. However, documents alone cannot prove consistent performance. Speak with recent customers if possible, and request a small pilot order before committing to volume. A slightly higher price may protect your schedule when sourcing, assembly, and quality control work together.

How to Choose a PCB Manufacturing and Assembly Partner

Benchmark comparison of typical partner profiles across pricing, lead times, communication, and supply chain support

Scores use a 0–100 evaluation scale: higher pricing scores indicate better cost efficiency, while higher scores for the other criteria indicate stronger performance. The benchmark reflects common sourcing priorities for prototype, low-volume, and high-volume PCB programs; actual results depend on board complexity, materials, order volume, testing requirements, and logistics.

Select the Partner and Establish Clear Project Agreements

How to Choose a PCB Manufacturing and Assembly Partner?

Selecting a partner is only half the work. Clear project agreements prevent expensive misunderstandings later. IPC’s 2024 Electronics Industry Survey identifies material availability, quality, and delivery as persistent industry concerns. Therefore, evaluate more than equipment lists. Ask for recent yield data, inspection methods, traceability records, and corrective-action examples. A capable partner should explain process limits in plain language. Request a written quotation covering tooling, testing, component substitutions, packaging, and shipping terms. I have seen projects fail because “standard tolerance” meant different things to each team.

Define acceptance criteria before production begins. Include layer count, impedance targets, surface finish, soldering standards, sampling plans, and change-control procedures. The electronics manufacturing sector increasingly depends on documented supply-chain visibility, according to recent IPC supply-chain surveys. Ask how the partner reports shortages, obsolete parts, and schedule risks. Set response times for technical questions. Also specify who approves engineering changes. A perfect agreement is unrealistic. A reviewable agreement is essential.

Tips:

Begin with a small pilot order and inspect first-article samples. Compare promised yield with actual results. Keep revision-controlled drawings in one shared system. Record every deviation, even minor ones. Do not rely on verbal approvals. A short weekly meeting can expose risks early, but meeting notes must assign owners and deadlines. Review the agreement after the pilot; weak assumptions often appear only during production.